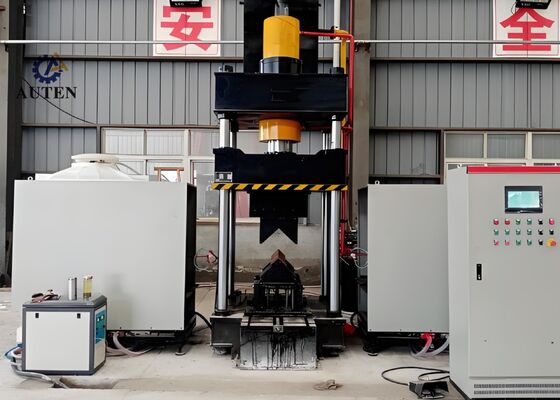
Model HQ250-700 CNC Angel Steel Bending And Heating Machine For Flat Metal Sheets
Product Introduction:
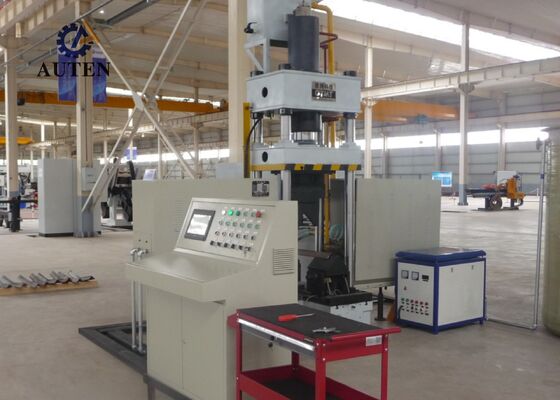
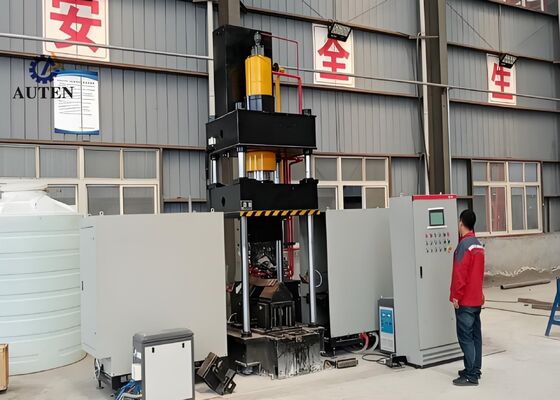
The CNC Thermal Bending System is professionally engineered and subjected to comprehensive factory testing to ensure accurate and reliable bending of angle steel profiles and flat metal sheets. It is specifically developed to meet the stringent manufacturing requirements of industries including structural steel fabrication, mechanical component production, and architectural metal processing. With excellent forming precision and consistent operating performance, the system ensures that processed angle steel and metal panels conform to demanding dimensional and structural requirements, supporting efficient and seamless execution of subsequent manufacturing operations.
Product parameters:
| Model |
HQ250-700 |
| Oil Tank Pressure (kN) |
1600 |
| Outside double-sided bending size (Heel up ) (mm) |
L80*7~L250*32 |
| Outward double-sided bending degree for angles (°) |
30° |
| Angle steel forward single bending range (mm) |
L80*7~L200*20 |
| Angle steel forward single bending degree (°) |
20° |
| Bending Plate thickness (mm) |
2~16 |
| Bending Plate width (mm) |
700 |
| Bending degree for plates (°) |
90° |
| Angle opening & closing range (mm) |
L80*7~L200*16 |
| Angle opening & closing degree (°) |
16° |
| Oil Tank Stroke (mm) |
800 |
| Max.opening height (mm) |
1300 |
| Motor Power (kW) |
15 |
| Heating power (kW) |
60*2 |
| CNC Axis |
3 |
| Oil tank capacity (L) |
630 |
| Overall size (m) |
3.5x4.5x4.1 |

Product Features:
1. The system integrates an advanced CNC-based PLC control platform with an intuitive touchscreen Human–Machine Interface (HMI), enabling convenient process parameter configuration, real-time equipment status monitoring, and efficient production management. This intelligent control system provides operators with a straightforward, dependable, and user-oriented operating environment.
2. The machine incorporates advanced ultrasonic-frequency induction heating technology to achieve rapid, uniform heating with improved energy utilization and reduced environmental impact. This efficient heating method helps increase production output, lower operating expenses, and meet applicable environmental protection requirements.
3. Designed as an integrated forming system, the equipment eliminates the need for additional tooling changes and frequent die adjustments. This simplified configuration reduces setup requirements, shortens preparation time, and improves overall production efficiency.
4. The machine utilizes precision CNC control technology to perform accurate bending and forming operations. It ensures consistent forming quality, precise dimensional control, and stable processing results while increasing manufacturing productivity.
5. An independent hydraulic power unit is integrated with a dedicated electrical control system to ensure convenient operation, enhanced safety, and stable equipment performance. This configuration is well suited to continuous operation in demanding industrial production environments.
6. In cold-forming mode, the machine can process angle steel sections up to L100 × L100 × 10 mm, with a maximum bending angle of 5°. This capability enables controlled material deformation and consistent forming precision within the specified operating range.
7. Under normal operating conditions, the cold-pressing cycle takes approximately 10 seconds per workpiece, whereas thermal bending generally requires around 120 seconds per component. Actual processing times depend on material properties and workpiece dimensions. Thermal bending begins when the workpiece reaches approximately 800°C and exhibits a red-hot appearance, with specific process settings adjusted according to the material characteristics and required forming accuracy.
8. For thermal bending operations, the operator simply enters the required processing parameters and initiates the automatic cycle using the control button or foot pedal switch. The machine then completes the programmed sequence automatically, including workpiece feeding into the heating zone, induction heating, automatic retraction of the heating unit, hydraulic clamping and pressing, ram lifting, and finished-workpiece discharge.
9. During combined thermal-forming and cold-pressing operations, the production cycle can begin as soon as the required parameters have been entered. Following the forming operation, the hydraulic ram does not need to return completely to its initial position. Instead, the lower pressing die automatically rises to provide a clearance of 100 mm, allowing the finished workpiece to be removed conveniently. This optimized operating sequence shortens the production cycle and further enhances overall manufacturing efficiency.
These test samples, produced using angle steel punching, cutting, and marking equipment, conform to the standard specifications and processing parameters commonly used in angle steel tower manufacturing. They provide customers with practical reference workpieces for assessing machining quality, dimensional accuracy, and manufacturing workmanship. These measurable indicators help demonstrate the equipment's ability to satisfy the demanding production requirements of angle steel tower fabrication.
In ultra-high-voltage (UHV) transmission line construction, transmission towers must withstand challenging environmental conditions and substantial structural loads. The equipment plays an important role in manufacturing the angle steel components that form the towers' primary load-bearing structures. It performs reliable drilling and punching operations on angle steel members used in tower bodies, cross-arms, and other critical structural sections, helping achieve accurate dimensions and dependable structural integrity. These processing capabilities contribute to the durability of transmission towers and support the safe, stable, and continuous operation of UHV power transmission systems.

 Your message must be between 20-3,000 characters!