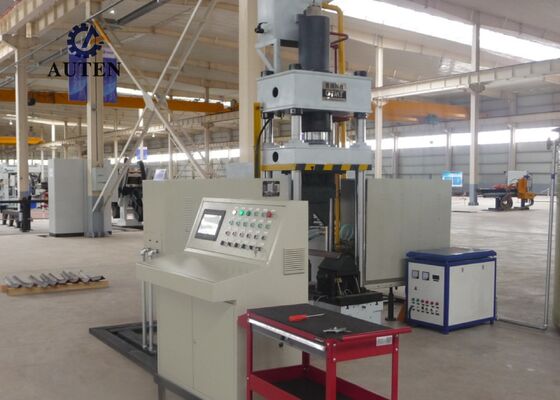
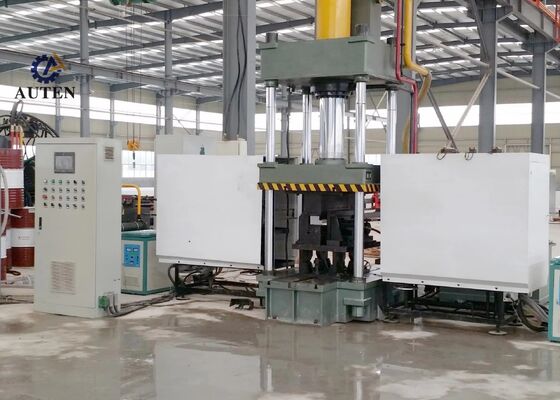
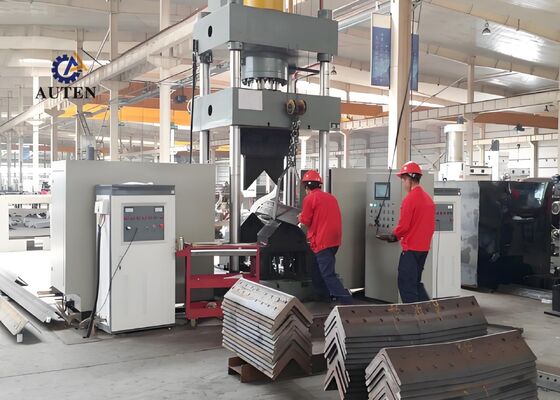
60*2KW Heating power CNC Angel Steel Bending And Heating Machine 1300mm Max. opening height
Product Introduction:
The CNC Thermal Bending System is professionally engineered and subjected to comprehensive factory testing to ensure accurate and reliable bending of angle steel profiles and flat metal sheets. It is specifically developed to meet the stringent manufacturing requirements of industries including structural steel fabrication, mechanical component production, and architectural metal processing. With excellent forming precision and consistent operating performance, the system ensures that processed angle steel and metal panels conform to demanding dimensional and structural requirements, supporting efficient and seamless execution of subsequent manufacturing operations.
Product parameters:
| Model |
HQ250-700 |
| Oil Tank Pressure (kN) |
1600 |
| Outside double-sided bending size (Heel up ) (mm) |
L80*7~L250*32 |
| Outward double-sided bending degree for angles (°) |
30° |
| Angle steel forward single bending range (mm) |
L80*7~L200*20 |
| Angle steel forward single bending degree (°) |
20° |
| Bending Plate thickness (mm) |
2~16 |
| Bending Plate width (mm) |
700 |
| Bending degree for plates (°) |
90° |
| Angle opening & closing range (mm) |
L80*7~L200*16 |
| Angle opening & closing degree (°) |
16° |
| Oil Tank Stroke (mm) |
800 |
| Max.opening height (mm) |
1300 |
| Motor Power (kW) |
15 |
| Heating power (kW) |
60*2 |
| CNC Axis |
3 |
| Oil tank capacity (L) |
630 |
| Overall size (m) |
3.5x4.5x4.1 |

Product Features:
1. The equipment is equipped with an advanced CNC and PLC-based control system featuring an intuitive touchscreen human–machine interface (HMI). It enables convenient configuration of processing parameters, real-time monitoring of machine status, and streamlined production management, providing operators with an accessible, reliable, and efficient operating environment.
2. The machine employs advanced ultrasonic-frequency induction heating technology to deliver rapid and uniform heating with enhanced energy efficiency and reduced environmental impact. This heating method supports increased production capacity, lower operating costs, and compliance with applicable environmental protection requirements.
3. The equipment features an integrated forming design that eliminates the need for additional tooling replacement and frequent die adjustments. This streamlined configuration reduces setup procedures, minimizes preparation time, and improves overall manufacturing efficiency.
4. By incorporating precision CNC control technology, the machine performs accurate bending and forming operations with consistent quality, precise dimensional control, and repeatable processing results, while enhancing overall production productivity.
5. The system integrates an independent hydraulic power unit with a dedicated electrical control system, ensuring convenient operation, improved operational safety, and dependable machine performance. This configuration is suitable for continuous production in demanding industrial environments.
6. In cold-forming mode, the machine accommodates angle steel profiles up to L100 × L100 × 10 mm and supports a maximum bending angle of 5°. Within the specified operating range, it enables controlled material deformation and consistent forming accuracy.
7. Under standard operating conditions, the cold-pressing cycle takes approximately 10 seconds per workpiece, while thermal bending generally requires about 120 seconds per component. Actual cycle times vary according to material properties and workpiece dimensions. Thermal bending typically begins when the material reaches approximately 800°C and exhibits a red-hot appearance. The specific heating and forming parameters should be adjusted to suit the material characteristics and required dimensional accuracy.
8. For thermal bending operations, the operator enters the required processing parameters and initiates the automatic cycle using the control button or foot pedal switch. The machine then executes the programmed sequence, including workpiece feeding into the heating zone, induction heating, automatic withdrawal of the heating unit, hydraulic clamping and pressing, ram lifting, and discharge of the finished workpiece.
9. During combined thermal-forming and cold-pressing operations, the production cycle can be initiated once the required parameters have been configured. After forming is completed, the hydraulic ram does not need to return fully to its original position. Instead, the lower pressing die automatically rises to create a clearance of 100 mm, facilitating convenient removal of the finished workpiece. This optimized sequence reduces cycle time and further improves overall production efficiency.
These test samples, produced using angle steel punching, cutting, and marking equipment, conform to the standard specifications and processing parameters commonly used in angle steel tower manufacturing. They provide customers with practical reference workpieces for assessing machining quality, dimensional accuracy, and manufacturing workmanship. These measurable indicators help demonstrate the equipment's ability to satisfy the demanding production requirements of angle steel tower fabrication.
In ultra-high-voltage (UHV) transmission line construction, transmission towers must withstand challenging environmental conditions and substantial structural loads. The equipment plays an important role in manufacturing the angle steel components that form the towers' primary load-bearing structures. It performs reliable drilling and punching operations on angle steel members used in tower bodies, cross-arms, and other critical structural sections, helping achieve accurate dimensions and dependable structural integrity. These processing capabilities contribute to the durability of transmission towers and support the safe, stable, and continuous operation of UHV power transmission systems.

 Your message must be between 20-3,000 characters!