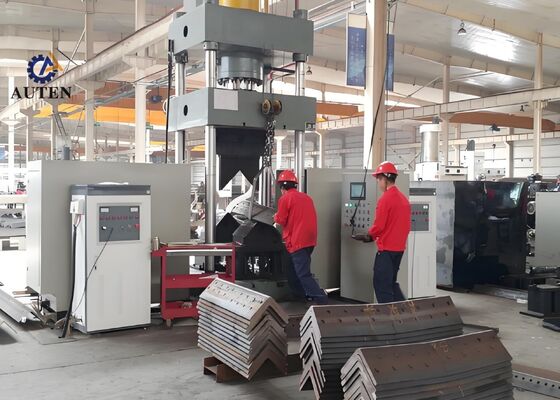
1600kN Oil Tank Pressure CNC Angle Bending Notching Milling Machine For Angle Steel Bending Task
Product Introduction:
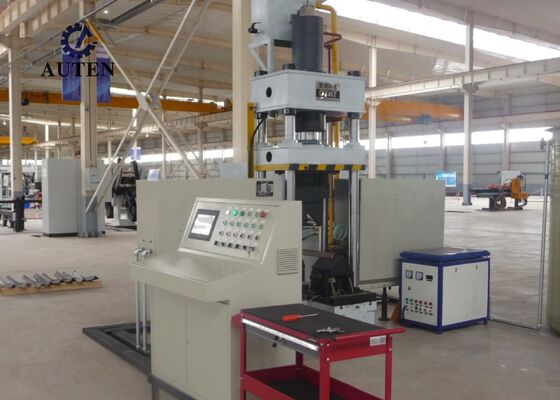
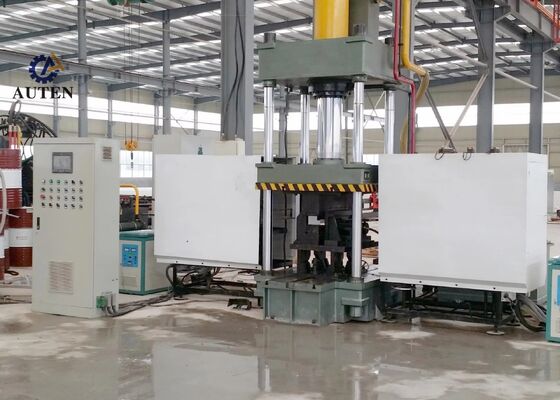
The CNC Thermal Bending System is professionally engineered and subjected to comprehensive factory testing to ensure accurate and reliable bending of angle steel profiles and flat metal sheets. It is specifically developed to meet the stringent manufacturing requirements of industries including structural steel fabrication, mechanical component production, and architectural metal processing. With excellent forming precision and consistent operating performance, the system ensures that processed angle steel and metal panels conform to demanding dimensional and structural requirements, supporting efficient and seamless execution of subsequent manufacturing operations.
Product parameters:
| Model |
HQ250-700 |
| Oil Tank Pressure (kN) |
1600 |
| Outside double-sided bending size (Heel up ) (mm) |
L80*7~L250*32 |
| Outward double-sided bending degree for angles (°) |
30° |
| Angle steel forward single bending range (mm) |
L80*7~L200*20 |
| Angle steel forward single bending degree (°) |
20° |
| Bending Plate thickness (mm) |
2~16 |
| Bending Plate width (mm) |
700 |
| Bending degree for plates (°) |
90° |
| Angle opening & closing range (mm) |
L80*7~L200*16 |
| Angle opening & closing degree (°) |
16° |
| Oil Tank Stroke (mm) |
800 |
| Max.opening height (mm) |
1300 |
| Motor Power (kW) |
15 |
| Heating power (kW) |
60*2 |
| CNC Axis |
3 |
| Oil tank capacity (L) |
630 |
| Overall size (m) |
3.5x4.5x4.1 |

Product Features:
1. The equipment incorporates an advanced CNC and PLC control system with an intuitive touchscreen human–machine interface (HMI). Operators can easily set processing parameters, monitor machine operating conditions in real time, and manage production tasks efficiently, ensuring a user-friendly, dependable, and productive operating experience.
2. The machine utilizes high-frequency ultrasonic induction heating technology to achieve rapid, uniform heating while improving energy utilization and reducing environmental impact. This heating solution helps increase production output, decrease operating expenses, and meet relevant environmental protection standards.
3. The equipment adopts an integrated forming configuration that removes the requirement for additional tooling changes and frequent die adjustments. This design simplifies setup procedures, shortens preparation time, and enhances overall production efficiency.
4. With precision CNC control, the machine performs bending and forming operations with high accuracy, consistent product quality, reliable dimensional control, and repeatable processing results, contributing to improved manufacturing productivity.
5. The system combines a dedicated hydraulic power unit with an independent electrical control system, providing convenient operation, enhanced safety, and stable equipment performance. This configuration is well suited to continuous operation in demanding industrial production environments.
6. In cold-forming mode, the machine can process angle steel up to L100 × L100 × 10 mm, with a maximum bending angle of 5°. Within the specified operating range, it ensures controlled deformation and consistent forming precision.
7. Under normal operating conditions, each cold-pressing cycle takes approximately 10 seconds, while thermal bending typically requires around 120 seconds per workpiece. Actual processing times depend on material characteristics and workpiece dimensions. Thermal bending generally begins when the material reaches approximately 800°C and becomes visibly red-hot. Heating and forming parameters should be appropriately adjusted according to the material properties and required dimensional tolerances.
8. For thermal bending, the operator enters the required processing settings and starts the automatic cycle using the control button or foot pedal switch. The machine then carries out the programmed sequence, including feeding the workpiece into the heating area, induction heating, automatic retraction of the heating unit, hydraulic clamping and pressing, ram elevation, and finished-workpiece discharge.
9. For combined thermal forming and cold pressing, the operating cycle begins after the required parameters have been configured. Once forming is complete, the hydraulic ram does not need to return completely to its initial position. Instead, the lower pressing die automatically rises to provide a clearance of 100 mm, allowing the finished workpiece to be removed conveniently. This optimized movement sequence shortens the production cycle and further increases overall processing efficiency.
These test samples, manufactured using angle steel punching, cutting, and marking equipment, reflect the standard dimensions and processing requirements commonly applied in angle steel transmission tower production. They serve as practical reference components for customers evaluating machining quality, dimensional precision, and manufacturing standards. Their measurable characteristics demonstrate the equipment's capability to meet the demanding production requirements of angle steel tower fabrication.
In ultra-high-voltage (UHV) transmission line projects, transmission towers must endure harsh environmental conditions and considerable structural loads. This equipment supports the production of angle steel components that constitute the primary load-bearing framework of these towers. It performs precise drilling and punching operations on angle steel members used in tower bodies, cross-arms, and other essential structural assemblies, helping maintain dimensional accuracy and reliable structural connections. These machining capabilities contribute to tower durability and support the safe, stable, and uninterrupted operation of UHV power transmission systems.

 Your message must be between 20-3,000 characters!