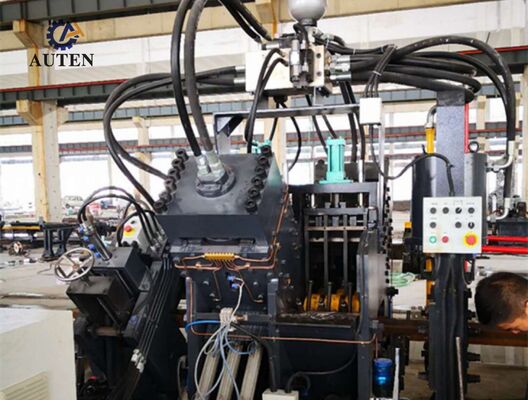
JNC1010 CNC Angle Punching Machine For Long Length Angle Steel Processing Up To 12 Meters
Product Introduction:
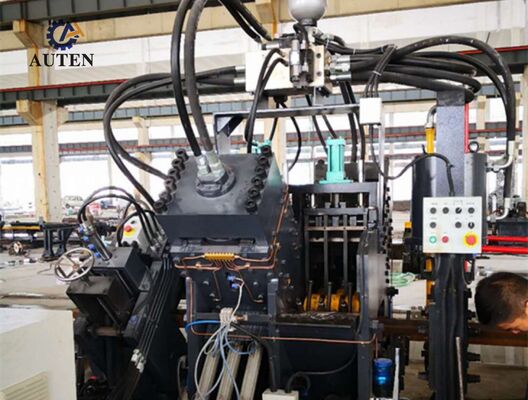
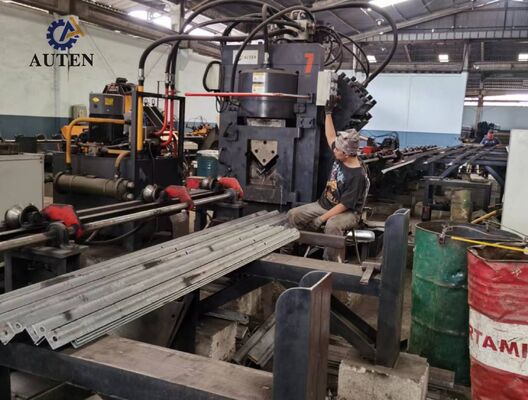
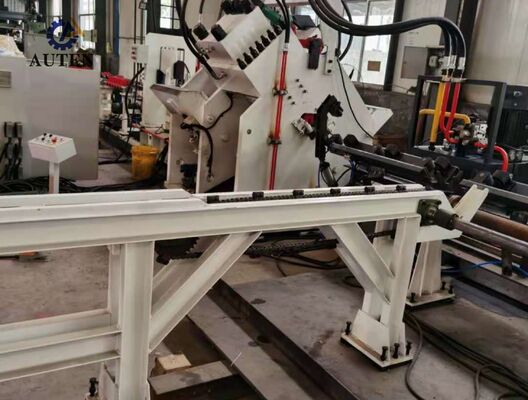
This equipment is specifically designed for punching, marking, and shearing angle steel used in power transmission tower production, structural steel manufacturing, and construction applications.
Product parameters:
| Model |
JNC1010 |
| Angle size (mm) |
40х40х3~100х100х10 |
| Max. Punching (Dia. х Thi.) (mm) |
Φ26х10 |
| Punching force (kN) |
630 |
| Marking force (kN) |
630 |
| Cutting force (kN) |
1000 |
| Max. length of blank (m) |
12 |
| Max. length of finished (m) |
8 |
| Punches per side |
2 |
| Group of marking letters |
4 |
| Number of letters per group |
12 |
| Character size(mm) |
14x10x19 |
| CNC axes |
3 |
| Cutting mode |
Single Blade |
| Cooling method |
Water cooling/Air cooling/Oil chiller |
| Max. feeding speed (m/min) |
80 |
| Programming mode |
Lofting software or instruction programming |
| Overall dimension (m) |
About 25x6.5x2.5 |
| The above parameters can be adjusted and changed according to customer's specific requirements. |

Product Features:
1. The machine combines advanced CNC technology with a servo-controlled feeding mechanism to achieve high production capacity and reliable machining accuracy. Major hydraulic, pneumatic, and electrical components are sourced from internationally recognized manufacturers, supporting dependable operation and consistent equipment performance.
2. Two or three punching stations are installed on each side of the machine, with each station accommodating three different punch diameters. This multi-tool arrangement allows various hole patterns to be completed in one setup, increasing processing efficiency and reducing the need for repeated workpiece repositioning.
3. The CNC feeding trolley is powered by an AC servo motor and equipped with a photoelectric encoder for continuous position detection. The closed-loop feedback system ensures precise positioning and repeatable material feeding throughout the machining process.
4. An industrial computer with a bilingual Chinese/English interface provides straightforward operation and clear graphical displays of workpiece drawings. The programming system supports both manual entry of machining parameters and processing data imported from specialized steel structure detailing software, accommodating a wide range of production needs.
5. The CNC feeding carriage employs servo-controlled movement integrated with photoelectric encoder feedback. This closed-loop positioning design ensures accurate workpiece alignment and stable feeding precision throughout each machining cycle.
6. Punching, marking, and shearing processes are carried out automatically. Once machining is complete, the finished angle steel profiles are unloaded by a pneumatic turnover device, reducing manual intervention and enhancing overall production efficiency.
7. The marking assembly features a robust, enclosed-frame structure designed to maintain rigidity and operational stability. It is equipped with four character-box assemblies, which are automatically selected according to the programmed marking requirements.
8. An optional shearing unit can be configured to cut angle steel profiles to designated lengths, providing greater flexibility for different fabrication specifications and production requirements.
9. The control system comprises an industrial computer, CNC controller, servo motors, PLC, and detection switches. After the workpiece drawing information is entered, the system automatically generates the corresponding machining program, streamlining programming procedures and reducing production setup time.
10. The hydraulic system supplies the operating force required for punching, shearing, marking, workpiece clamping, and character-box replacement. These coordinated hydraulic functions facilitate integrated machining operations and support continuous automated production.
These sample workpieces illustrate commonly used specifications and representative processing requirements in angle steel tower fabrication. They provide customers with practical examples for assessing machining quality, dimensional precision, and manufacturing standards. By offering a direct reference for evaluating equipment capabilities and conformance to production requirements, the samples help facilitate objective machine assessment and well-informed purchasing decisions.
In ultra-high-voltage (UHV) transmission line projects, transmission towers are required to withstand demanding weather conditions and considerable structural loads. This equipment supports the production of angle steel components that constitute the main structural framework of these towers. It carries out consistent punching and marking operations on angle steel members used in tower bodies, cross-arms, and other essential structural sections. Accurate hole positioning and consistent dimensions help ensure dependable component assembly and contribute to the structural integrity and operational stability of transmission towers.

 Your message must be between 20-3,000 characters!