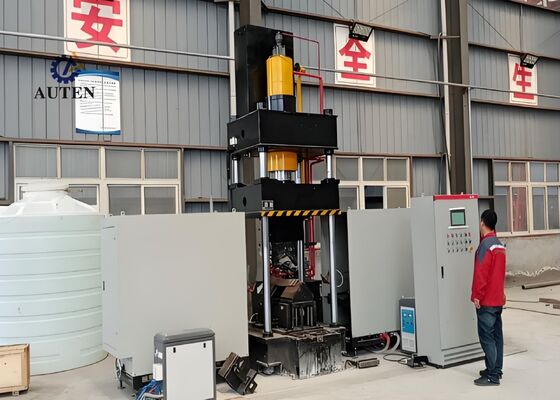
Heavy Duty CNC Heating Bending Machine For Angle & Plate For Steel Tower Fabrication
Product Introduction:
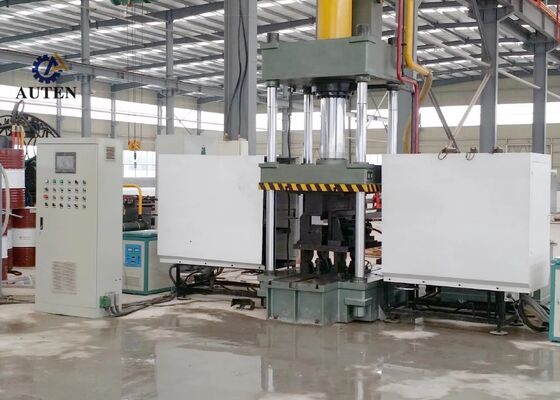
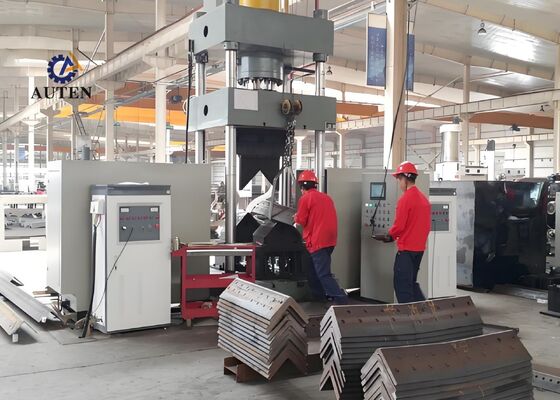
The CNC Thermal Bending System is professionally engineered and subjected to comprehensive factory testing to ensure accurate and reliable bending of angle steel profiles and flat metal sheets. It is specifically developed to meet the stringent manufacturing requirements of industries including structural steel fabrication, mechanical component production, and architectural metal processing. With excellent forming precision and consistent operating performance, the system ensures that processed angle steel and metal panels conform to demanding dimensional and structural requirements, supporting efficient and seamless execution of subsequent manufacturing operations.
Product parameters:
| Model |
HQ250-700 |
| Oil Tank Pressure (kN) |
1600 |
| Outside double-sided bending size (Heel up ) (mm) |
L80*7~L250*32 |
| Outward double-sided bending degree for angles (°) |
30° |
| Angle steel forward single bending range (mm) |
L80*7~L200*20 |
| Angle steel forward single bending degree (°) |
20° |
| Bending Plate thickness (mm) |
2~16 |
| Bending Plate width (mm) |
700 |
| Bending degree for plates (°) |
90° |
| Angle opening & closing range (mm) |
L80*7~L200*16 |
| Angle opening & closing degree (°) |
16° |
| Oil Tank Stroke (mm) |
800 |
| Max.opening height (mm) |
1300 |
| Motor Power (kW) |
15 |
| Heating power (kW) |
60*2 |
| CNC Axis |
3 |
| Oil tank capacity (L) |
630 |
| Overall size (m) |
3.5x4.5x4.1 |

Product Features:
1. The machine is equipped with an advanced CNC and PLC-based control system, complemented by an intuitive touchscreen Human–Machine Interface (HMI). Operators can conveniently configure processing parameters, monitor equipment status in real time, and coordinate production operations, ensuring straightforward operation, reliable performance, and efficient workflow management.
2. The equipment employs high-frequency ultrasonic induction heating technology to provide fast and consistent heating, optimize energy consumption, and minimize environmental impact. This advanced heating method helps improve production capacity, reduce operating costs, and comply with applicable environmental protection requirements.
3. The machine features an integrated forming system that eliminates the need for additional tooling replacement and frequent die adjustments. This streamlined configuration simplifies equipment setup, reduces production preparation time, and improves overall operational efficiency.
4. Equipped with precision CNC control technology, the machine delivers accurate bending and forming performance, uniform product quality, precise dimensional control, and highly repeatable processing results, thereby enhancing overall manufacturing efficiency.
5. The equipment integrates a dedicated hydraulic power station with an independent electrical control system, ensuring convenient operation, improved operational safety, and consistent machine performance. This arrangement is particularly suitable for continuous production under demanding industrial working conditions.
6. In cold-forming operation, the machine is capable of processing angle steel profiles up to L100 × L100 × 10 mm, with a maximum allowable bending angle of 5°. Within this specified capacity range, the equipment provides controlled material deformation and stable forming accuracy.
7. Under standard operating conditions, the cold-pressing cycle takes approximately 10 seconds per workpiece, whereas thermal bending generally requires approximately 120 seconds. The actual cycle time varies according to material properties and workpiece dimensions. Thermal forming typically commences when the material reaches approximately 800°C and exhibits a red-hot appearance. Heating and forming parameters are adjusted as necessary to accommodate material characteristics and specified dimensional tolerances.
8. During thermal bending operations, the operator only needs to input the required processing parameters and activate the automatic cycle through the control button or foot pedal switch. The machine subsequently executes the complete programmed sequence, including workpiece positioning in the heating zone, induction heating, automatic withdrawal of the heating unit, hydraulic clamping and pressing, ram return movement, and discharge of the finished component.
9. In the combined thermal forming and cold-pressing mode, the production cycle starts once all required parameters have been configured. After forming is completed, the hydraulic ram does not need to return fully to its original position. Instead, the lower pressing die automatically moves upward to create a clearance of approximately 100 mm, facilitating convenient removal of the finished workpiece. This optimized operating sequence reduces cycle time and further enhances overall production efficiency.
These demonstration samples are produced using angle steel punching, cutting, and marking equipment and represent the standard dimensions and typical processing specifications used in angle steel transmission tower manufacturing. They provide practical reference components for customers to assess machining quality, dimensional accuracy, and manufacturing workmanship. Through these finished samples, prospective buyers can evaluate the equipment's ability to satisfy the stringent processing and production requirements of angle steel tower fabrication.
In ultra-high-voltage (UHV) transmission line projects, transmission towers are required to withstand severe environmental conditions and substantial structural loads throughout their service life. This equipment plays an important role in manufacturing the angle steel components that form the primary load-bearing structures of these towers. It carries out precision drilling and punching operations on angle steel members used in tower bodies, cross-arms, and other critical structural assemblies, helping ensure accurate dimensions and dependable structural connections. These processing capabilities contribute to the overall durability of transmission towers while supporting the safe, stable, and continuous operation of UHV power transmission systems.

 Your message must be between 20-3,000 characters!