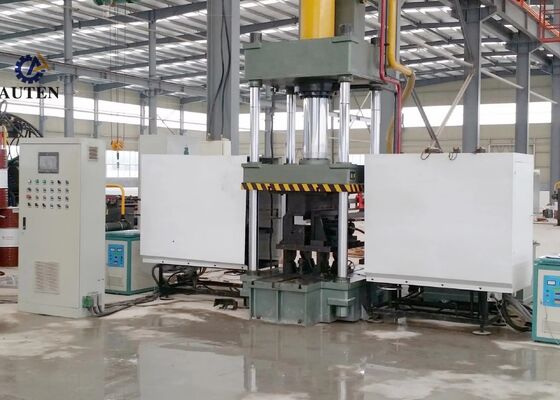
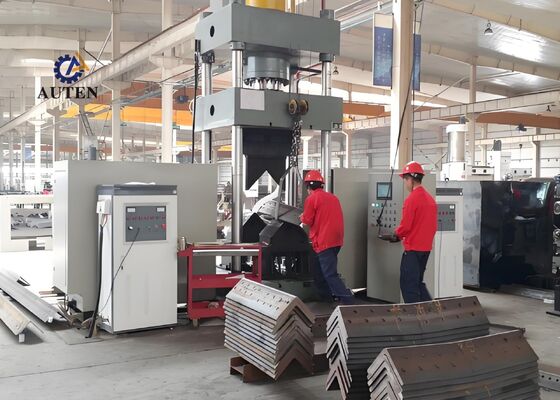
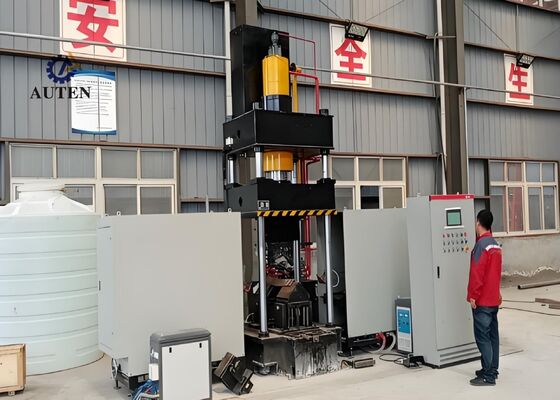
3150kN CNC Heating Bending Machine For Angle Steel And Plate With 240kW Heating Power
Product Introduction:
The CNC Thermal Bending System is professionally engineered and subjected to comprehensive factory testing to ensure accurate and reliable bending of angle steel profiles and flat metal sheets. It is specifically developed to meet the stringent manufacturing requirements of industries including structural steel fabrication, mechanical component production, and architectural metal processing. With excellent forming precision and consistent operating performance, the system ensures that processed angle steel and metal panels conform to demanding dimensional and structural requirements, supporting efficient and seamless execution of subsequent manufacturing operations.
Product parameters:
| Model |
HQ250-700 |
| Oil Tank Pressure (kN) |
1600 |
| Outside double-sided bending size (Heel up ) (mm) |
L80*7~L250*32 |
| Outward double-sided bending degree for angles (°) |
30° |
| Angle steel forward single bending range (mm) |
L80*7~L200*20 |
| Angle steel forward single bending degree (°) |
20° |
| Bending Plate thickness (mm) |
2~16 |
| Bending Plate width (mm) |
700 |
| Bending degree for plates (°) |
90° |
| Angle opening & closing range (mm) |
L80*7~L200*16 |
| Angle opening & closing degree (°) |
16° |
| Oil Tank Stroke (mm) |
800 |
| Max.opening height (mm) |
1300 |
| Motor Power (kW) |
15 |
| Heating power (kW) |
60*2 |
| CNC Axis |
3 |
| Oil tank capacity (L) |
630 |
| Overall size (m) |
3.5x4.5x4.1 |

Product Features:
1. The machine adopts an advanced CNC and PLC integrated control system, featuring a user-friendly touchscreen Human–Machine Interface (HMI). Operators can easily set processing parameters, monitor machine operating conditions in real time, and manage production procedures efficiently. This configuration ensures convenient operation, dependable equipment performance, and streamlined production management.
2. The equipment utilizes high-frequency ultrasonic induction heating technology to achieve rapid, uniform heating while improving energy efficiency and reducing environmental impact. This heating method helps increase production output, lower operating expenses, and meet relevant environmental protection standards.
3. The machine incorporates an integrated forming system that removes the requirement for additional tooling changes and repeated die adjustments. This simplified design makes machine preparation more convenient, shortens setup time, and enhances overall production efficiency.
4. With precise CNC control technology, the machine ensures accurate bending and forming operations, consistent product quality, reliable dimensional accuracy, and repeatable processing results, contributing to improved manufacturing productivity.
5. The equipment is designed with a dedicated hydraulic power unit and a separate electrical control system, providing convenient operation, enhanced safety, and stable operating performance. This configuration is well suited to continuous manufacturing processes and demanding industrial production environments.
6. In cold-forming mode, the machine can process angle steel sections up to L100 × L100 × 10 mm, with a maximum bending angle of 5°. Within this rated processing range, it maintains controlled material deformation and consistent forming precision.
7. Under normal working conditions, the cold-pressing cycle requires approximately 10 seconds per workpiece, while the thermal bending cycle takes around 120 seconds. Actual processing times depend on the material characteristics and workpiece dimensions. Thermal forming generally begins when the material reaches approximately 800°C and becomes visibly red-hot. Heating and forming settings can be adjusted according to material properties and the required dimensional tolerances.
8. For thermal bending operations, the operator simply enters the required processing data and initiates the automatic cycle using the control button or foot pedal switch. The machine then completes the entire programmed process automatically, including positioning the workpiece in the heating area, induction heating, automatic retraction of the heating unit, hydraulic clamping and pressing, return movement of the ram, and unloading of the finished component.
9. When operating in the combined thermal forming and cold-pressing mode, production begins after the relevant processing parameters have been entered. Once forming is completed, the hydraulic ram is not required to return completely to its initial position. Instead, the lower pressing die automatically rises to provide an approximately 100 mm clearance, allowing the finished workpiece to be removed more easily. This optimized process shortens the operating cycle and improves overall production efficiency.
These demonstration samples are manufactured using angle steel punching, cutting, and marking equipment. They reflect the standard dimensions and typical processing requirements of angle steel components used in transmission tower production. The samples serve as practical reference parts, enabling customers to evaluate machining quality, dimensional precision, and manufacturing standards. By inspecting these finished components, prospective buyers can assess whether the equipment meets the demanding processing and production requirements of angle steel transmission tower fabrication.
For ultra-high-voltage (UHV) transmission line projects, transmission towers must withstand challenging environmental conditions and considerable structural loads throughout their operational service life. This equipment supports the production of angle steel components that constitute the main load-bearing framework of these towers. It performs precision drilling and punching operations on angle steel members used in tower structures, cross-arms, and other essential assemblies, helping maintain dimensional accuracy and reliable connection quality. These processing capabilities contribute to the structural strength and long-term durability of transmission towers, while supporting the safe, stable, and uninterrupted operation of UHV power transmission systems.

 Your message must be between 20-3,000 characters!