High Speed CNC Angle Steel Drilling Marking Machine Automatically For High Voltage Tower
Product Introduction:
The CNC Angle Steel Drilling, Marking and Shearing Line represents a sophisticated numerically controlled system engineered for the rapid, accurate and high-efficiency fabrication of angle steel within the steel structure sector. This automated production line consolidates drilling, marking and shearing processes into one unified workflow, substantially boosting throughput while cutting manual labour input and overall cycle time.
Fitted with a robust CNC control platform, the equipment guarantees precise positioning and repeatable machining outcomes. It supports angle steel of multiple specifications to satisfy varied project specifications. The drilling module achieves accurate hole layout, and the marking module creates legible identifiers to facilitate subsequent assembly. Its shearing module delivers neat, dimensionally accurate cuts for superior finished quality.
Widely deployed in building construction, power transmission tower manufacturing and general steel structure industries, this solution features stable performance, extended service life and outstanding operational efficiency. Its intelligent architecture and multi-process functionality render it a preferred option for contemporary production facilities prioritising precision and output capacity.
Main Parameters:
| Model |
ADM2532 |
| Angle size (mm) |
100×100×10~250×250×32 |
| Max. length of blank(m) |
14 |
| Taper of drilling spindle |
BT40 |
| Max. Drilling diameter (mm) |
Ф40 |
| Qty. of drill on each side (pcs) |
3 (6 in total on both side) |
| Max.spindle rotation speed (r/min) |
6000 |
| Max.cutting speed of drill (m/min) |
200 |
| CNC axes |
9 |
| Range of back mark (mm) |
50-220 (stepless) |
| Max. angle feeding speed (m/min) |
40 |
| Marking force (kN) |
1000/1200 |
| Qty. of character group |
4 |
| Qty. of character in each group |
18 |
| Character size(mm) |
14×10×19 |
| Drill bit cooling system |
Air atomization dry internal cooling |
| Programming mode |
Lofting software or instruction programming |
| Overall dimensions (m) |
34×8×3 |

Product Features:
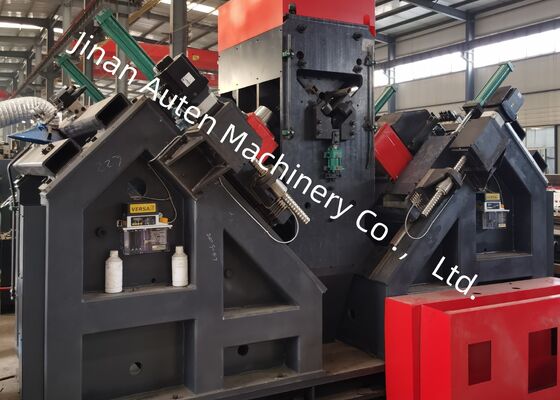
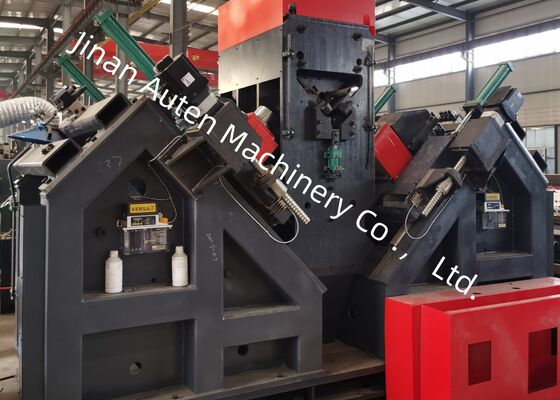
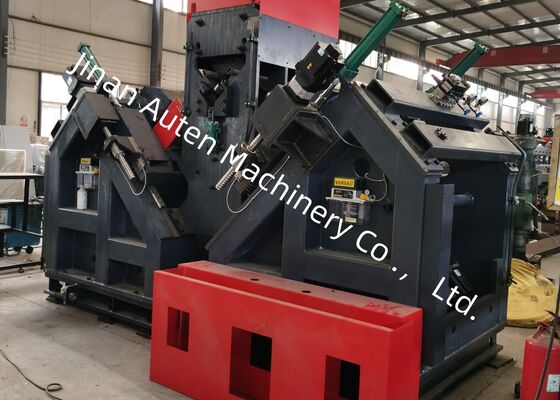
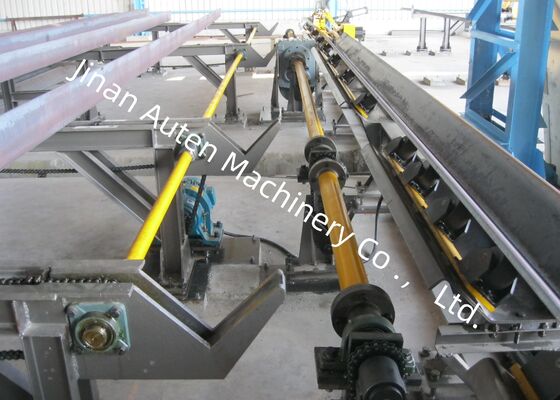
1. The full production line comprises cross conveyors, turnover conveyors, feeding conveyors, CNC feeding trolleys, two drilling stations, one marking station, an automatic discharge conveyor, a hydraulic power unit and an electrical cooling system. Incorporating state-of-the-art CNC technology and servo material feeding, the equipment achieves high processing throughput, stable running and uniform workpiece precision.
2. Drilling stations are arranged on both sides of the machine frame. Each station can hold three drills of distinct diameters. All drilling units are governed by the CNC system and capable of autonomous movement for hole pitch adjustment, securing accurate hole locations and consistent machining tolerance.
3. Spindle rotation speed adopts stepless regulation via a frequency converter, whereas feed speed is modulated by flow control valves. Automatic switching among fast advance, working feed and rapid retract is realised to enable smooth cycling and elevate processing efficiency.
4. This drilling line is configured with one marking station, whose marking spacing can be pre-set flexibly in accordance with production demands. Marking action, workpiece clamping and drilling feed are hydraulically actuated. Core components are sourced internationally to assure stable performance. A built-in recirculating cooling system suppresses cutting temperature and prolongs drill bit lifespan.
5. Marking and drilling sequences run fully automatically. Once machining is finished, finished angle steel sections are ejected by a pneumatic turnover mechanism. This design minimises manual material handling, alleviates labour intensity and delivers higher productivity relative to traditional processing setups.
6. The control framework integrates an industrial mainframe, servo motors, PLC, external detection switches and other vital control hardware. Operators simply input workpiece parameters, and the system will auto-generate the corresponding machining programme. Programmes can also be saved, recalled, previewed and retrieved by unique workpiece codes, simplifying shop-floor production administration.
7. The processing line is fitted with workpiece support and clamping assemblies, which can accommodate angle steel sections with notable bending or distortion. Such arrangement maintains secure positioning and dependable machining precision throughout the working cycle.
These demonstration workpieces cover a variety of standard dimensions and typical hole configurations commonly used in angle steel transmission tower fabrication. They provide prospective customers and quality inspection personnel with practical reference samples for evaluating machining accuracy, processing performance, and finished-component quality. By examining the actual processed workpieces, users can determine whether the equipment satisfies the relevant manufacturing standards and production specifications for transmission tower applications.
In ultra-high-voltage (UHV) transmission line projects, transmission towers must withstand harsh weather conditions and considerable structural loads. This equipment is designed to manufacture the angle steel components that constitute the primary load-bearing framework of these structures. It performs high-precision drilling and punching operations on angle steel members used in tower bodies, cross-arms, and other essential structural assemblies, helping maintain accurate dimensions and dependable connection points. These machining capabilities contribute to enhanced structural integrity, improved operational stability, and long-term service reliability throughout the intended operating life of transmission towers.

 Your message must be between 20-3,000 characters!